OEM Distribution Box Essentials: Design, Use Cases, and Best Practices
2026-09-22
Every switchboard and control panel hides a silent workhorse: the OEM distribution box. It routes power, protects circuits, and keeps field wiring tidy—yet it rarely gets the design attention it deserves. From compact machine tools to sprawling conveyor lines, the right enclosure can slash assembly time and prevent costly downtime. In this guide, we’ll break down what makes a distribution box truly OEM‑ready, explore real‑world use cases, and share best practices that go beyond the catalog spec sheet. Whether you’re prototyping or scaling production, ETEK’s engineering insights will help you avoid the usual pitfalls and build a panel that lasts.
What a Well-Built OEM Box Gets Right Before the First Wire Lands
The moment the box arrives, the difference is tactile. Cold-rolled steel panels meet with consistent corner radii, and every knockout aligns without forced persuasion. Threaded inserts sit flush instead of tilting under a wrench, because the supplier punches those holes after bending, not before. That sequence matters more than most engineers admit.
A powder coat gets all the credit, but what hides underneath does the real work. The phosphate underlayer prevents rust creep along cut edges, while the coating itself stays thin enough not to insulate the ground path. Inside, pre-tapped bosses for DIN rail and wire duct sit exactly where the layout drawing promised, leaving nothing to drill on site.
Small details accumulate before a single conductor is stripped. Hinges cycle without play after a thousand test openings, sealing gaskets arrive pre-seated in their grooves, and each opening wears a protective film until the last moment. Even the ground stud ships with a copper washer already in place. None of this shows up on a datasheet, but it all shows up on install day.
Enclosure Materials and Finishes That Outlast the Cheapest Quote
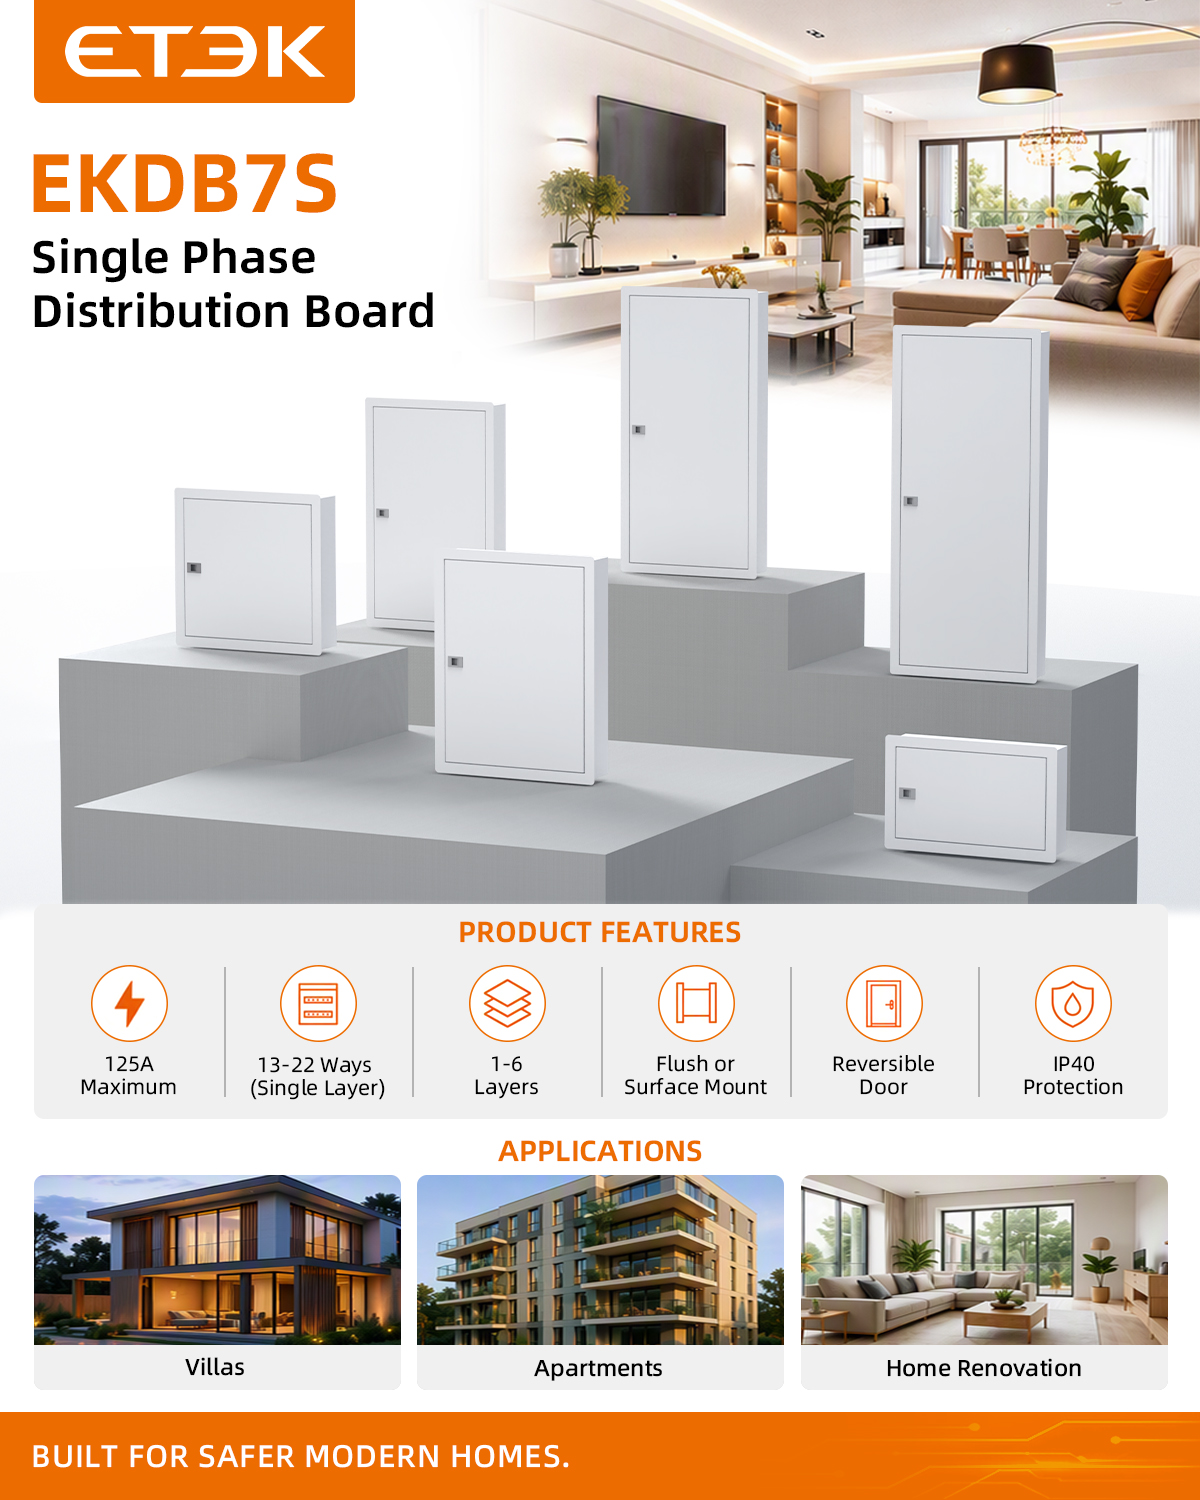
When the lowest bid wins, the first things to disappear are usually the details you can't see at a glance: thicker powder coating, marine-grade gaskets, or 316 stainless instead of 304. That's why we spec enclosures with finishes tied to the actual environment, not just the price sheet. A coastal installation gets electro-polished hardware and a salt-fog-rated coating; a washdown area gets passivated seams and sealed fasteners instead of raw cut edges that start rusting in six months.
The real cost difference shows up after a few seasons. Powder coat that's applied too thin chalks and peels, while UV-stable polyester topcoats keep their color and adhesion. Neoprene gaskets harden faster than EPDM or silicone when exposed to ozone or cleaning chemicals. Choosing materials that match the exposure isn't over-engineering, it's just the difference between replacing an enclosure once and replacing it every few years.
Busbar, Breaker, and Terminal Layouts That Keep Callbacks Rare
Most callbacks trace back to a handful of layout decisions made long before installation. Busbars that force tight bend radii near breaker lugs, breakers stacked without thermal derating, or terminals placed where torque wrenches barely fit all set the stage for nuisance trips and loose connections. A better approach starts with leaving enough straight busbar before the first bend—at least two times the bar width—so expansion and vibration don't concentrate stress at a single point. Breakers with similar frame sizes can share a common mounting rail, but their line-side terminals should never face a blank enclosure wall with less than four inches of clearance. That extra space lets inspectors verify lug torque without removing adjacent conductors, which reduces the chance of a future call for arcing or overheating.
Terminal placement gets overlooked because it doesn't show up on single-line diagrams. Yet field failures often begin where control wiring crosses power busbars, or where neutral and ground bars sit so close that a dropped washer bridges them during routine service. A practical layout puts power terminals on one vertical plane and control terminals on a separate DIN rail at least six inches away, with wire duct between them sized for the largest expected conductor plus 30 percent spare capacity. For breaker line and load connections, orient lugs so the cable approaches from below on line side and exits upward on load side—this creates a natural drip loop and keeps heat from collecting around the breaker body. If the enclosure is less than 24 inches wide, consider offsetting the main breaker from the branch breakers rather than centering it; the asymmetry looks less tidy but measurably improves airflow and reduces hot spots.
The real payoff shows up months later when a technician opens the panel for an unrelated issue and doesn't find discolored insulation, loose lugs, or a breaker handle that's warm to the touch. That's not luck; it's a layout that respects thermal expansion, wrench clearance, and the simple fact that wires move every time a breaker operates. Spending an extra hour on busbar routing and terminal grouping during design costs far less than one callback with an infrared camera and an unhappy customer. When every component can be reached without a mirror, and no conductor is forced into a radius tighter than the manufacturer's minimum, the phone stays quiet.
Use Cases Where the Distribution Box Disappears Into the Equipment
In high-end medical imaging equipment, the distribution box is often tucked directly into the gantry base or console housing, eliminating the separate wall-mounted panel altogether. Breakers, filters, and terminal blocks are rearranged inside a dedicated metal compartment within the machine, using the equipment's own airflow to manage heat. This approach spares the room from extra conduit runs and makes it far easier to reposition the device without rewiring the facility.
Modular data centers and compact robotic workstations take a similar route. The power distribution unit becomes a drawer-style module that sits flush with the cabinet front when closed, completely hiding its presence. A technician can slide the module out for servicing, while the closed position keeps live parts away from untrained staff. Because there is no separate distribution closet to allocate, both floor space and installation time shrink noticeably.
Installation and Wiring Choices That Protect the Entire Assembly
The way you route and terminate conductors determines whether the whole assembly behaves as a robust unit or a chain of weak links. Start by sizing wire insulation for the highest temperature and voltage spikes the system can see, not just the nominal ratings. Pre-formed harnesses with service loops at pivot points take stress off solder joints and terminal blocks, while coarse-thread screws with captive washers keep connection points from loosening under repeated thermal cycling. If the enclosure sees washdowns, use drip legs and downward-facing cable entries so moisture never pools against seals.
Separation matters more than many designers admit. Running low-level sensor lines in the same bundle as motor drives invites noise that zeroes out signal integrity, even when everything works on a bench test. Physical spacing, twisted pairs for differential signals, and grounded barriers between power and control sections cost very little during assembly but eliminate the intermittent faults that eat up field-service hours later. Label both ends of every conductor with durable, heat-shrink markers that stay legible after exposure to oil and sunlight.
Finally, build the assembly so it can be tested in place without cutting zip ties or peeling back loom. Bring out test points on a small, clearly marked rail, and leave enough slack for clamp-on current probes. This turns what is often a blind installation into one where the next technician can verify continuity, insulation resistance, and load balance in minutes, then close the panel with confidence that the whole assembly will hold up over years of real-world operation.
Routine Checks That Keep OEM Boxes Predictable Over a Decade
Most facilities treat an OEM box as a set-and-forget asset until something trips. That mindset is exactly what turns a five-minute inspection into a day-long rebuild. Predictability over ten years doesn't come from buying a premium enclosure—it comes from walking past it every week with a checklist and actually looking at the details.
The checks themselves are mundane but non-negotiable. Start with the gaskets and cable entries; a worn seal lets in dust that quietly coats circuit boards and accelerates corrosion. Then move to internal temperature and humidity logs. A slow rise in ambient temperature often signals a failing cooling fan or blocked vents long before an alarm triggers. For electrical connections, use a torque screwdriver on terminal blocks once a year—vibration loosens even properly torqued screws over time. And don't ignore the small stuff: door hinges, latch alignment, and the condition of the grounding strap. These are the parts that nobody notices until a door falls open during a rainstorm.
The real trick is consistency without drama. Keep a simple handwritten or spreadsheet log for each box, note every reading, and compare month-over-month trends. If a particular box runs 3°C hotter every summer, plan maintenance around that cycle instead of reacting to an emergency. After a few seasons, the routine becomes second nature and the box becomes boring—which is exactly what you want. A decade of boring weekly checks is far cheaper than one spectacular failure.
FAQ
Start with the enclosure material and sealing method. Powder-coated steel works for most indoor applications, but outdoor or washdown areas demand stainless steel or polycarbonate with a continuous gasket. Pay attention to thermal expansion of internal busbars, and always derate components for the highest expected ambient temperature rather than the average.
A purpose-built box eliminates unused space and adapts to the exact component layout, which shortens wire runs and reduces the chance of loose connections. It also lets you position heat-generating parts away from sensitive electronics and route cables so field technicians can reach test points without disassembling unrelated sections.
Mobile machinery, food processing lines, and modular automation cells see the biggest gains. These environments have tight space, frequent washdowns, or repeated reconfiguration, so a box that fits the machine envelope and meets the right ingress rating prevents failures a generic enclosure would invite.
Group components by voltage level and heat output, keep AC and DC wiring separated, and leave at least 20% spare room for future upgrades. Mount terminals on a rail near the cable entry points so field wiring doesn't cross over contactors or drives. Label every termination with the same identifier used in the schematic.
Add it when unplanned downtime costs more than the sensor and gateway hardware. Current transformers on main feeders, temperature probes near busbar joints, and a simple Modbus or IO-Link gateway let operators spot loose connections or overloaded phases before a failure. For low-cost machines, skip it; for high-value process equipment, it pays back quickly.
Designers often size fans for the total nameplate load instead of actual diversity, which leads to oversized cooling and dust ingress. Another mistake is placing the exhaust vent directly above a drive heatsink, recirculating hot air. Use vertical airflow paths, separate high-heat zones, and validate temperatures at full load and 10% above rated ambient.
Choose an IP rating based on actual exposure, not worst-case fear. IP54 is enough for most factory floors, while IP66 matters for outdoor or washdown. Use captive screws, hinged covers with stays, and gaskets that stay attached to the door. Put frequently accessed components, like resets and test points, behind a smaller secondary cover so the main seal isn't broken routinely.
Conclusion
A distribution box that earns its place on an OEM machine starts with decisions made long before the first conductor is terminated. Enclosure sizing accounts for heat load at full duty, not just component count. Materials matter in ways a datasheet won't advertise: powder-coated steel handles dry indoor panels, but a washdown line or outdoor skid often needs 316 stainless or fiberglass-reinforced polycarbonate because the gasket groove and hinge hardware fail before the metal does. Inside, busbar, breaker, and terminal placement determines whether a technician can torque a breaker lug without pulling four other wires out of the way. Generous wire bending radius, grouped neutral and ground bars, and breaker labels that match the schematic cut commissioning time. A layout that ignores thermal derating under a sealed cover will trip unexpectedly on a hot afternoon, even if every component looked fine on paper.
In practice, the best OEM boxes disappear into the equipment they serve. A compact distribution block mounted behind a robot controller or a swing-out panel inside a packaging machine keeps wiring short and protects the assembly from snags. That integration works only if installation choices are deliberate: ferrules on stranded wire, strain relief at every entry point, wire duct fill below 40 percent, and torque wrenches set to the manufacturer's spec rather than "tight enough." Over a decade, routine checks keep that predictability alive. Thermal imaging catches loose connections before they carbonize. Re-torquing after thermal cycling, checking enclosure seals for compression set, and verifying that filters or breathers aren't clogged cost minutes but avoid failures that stall a production line. The boxes that rarely call back are not built from a better bill of materials alone—they reflect a discipline that treats the panel as a system, not a box of parts.
Contact Us
Contact Person: Andy
Email: [email protected]
Tel/WhatsApp: +86 13356133008
Website: https://www.etek-china.com/