Bead Wire Ring Production Line Supplier Key Considerations for Your Next Purchase
2026-10-03
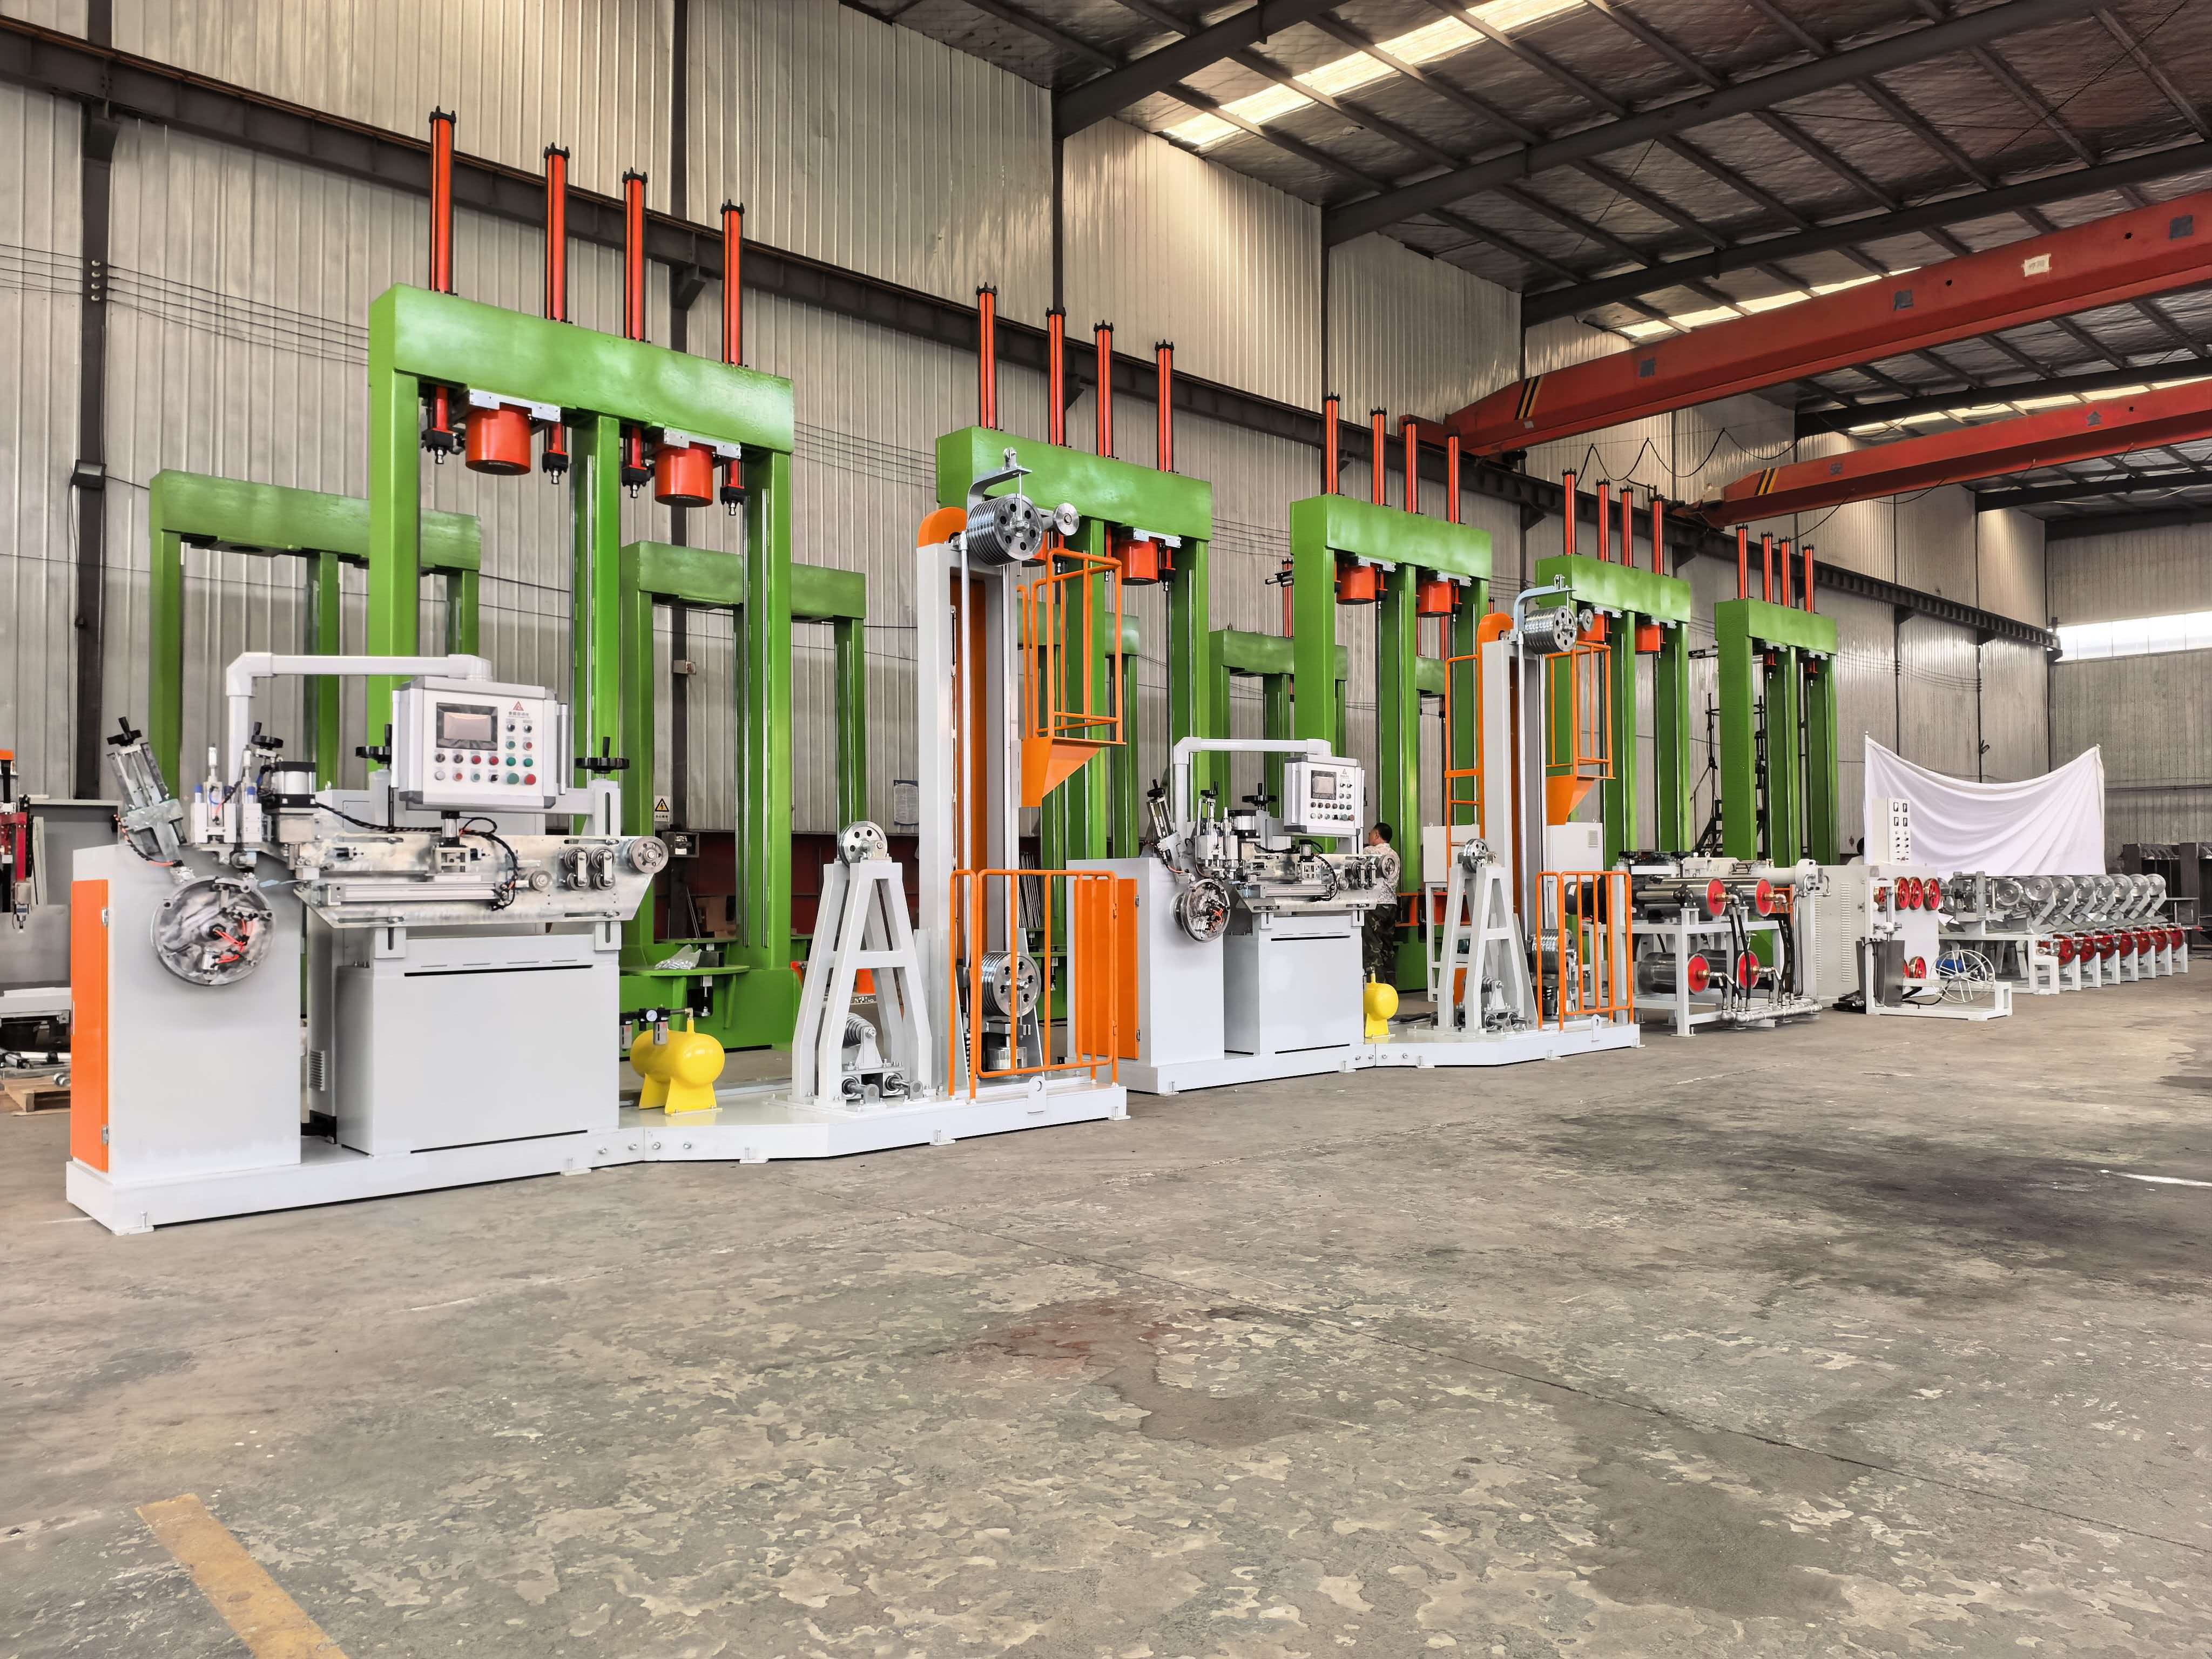
Investing in a bead wire ring production line is rarely a straightforward decision. From tension control and ring geometry to changeover speed and after-sales support, the gaps between suppliers are wider than most buyers expect. Before you shortlist vendors, it pays to look beyond spec sheets and ask where a line will struggle when your production mix shifts. That’s where a supplier like AUGU AUTOMATION tends to stand out—not just for equipment, but for the engineering judgment behind it. This guide covers the key considerations that should shape your next purchase.
Cut Through Sales Claims: Questions That Reveal True Line Capability
Sales sheets love to boast about cycle times, throughput, and flexibility, but those numbers rarely survive contact with your actual product mix. Instead of accepting the headline figure, ask what happens when the line runs your three most awkward SKUs back to back. Real capability shows up in changeover losses, starvation at the infeed, and the buffer logic that keeps a short stoppage from turning into a half-hour reset.
Push beyond the spec sheet by requesting a dry run with your own containers and labels, even if it means a slower pace. A line that handles a uniform demo product beautifully can fall apart when faced with tapered bottles, flimsy cartons, or a label that wrinkles at the slightest humidity. Ask the vendor to identify the two most common failure modes for their installed base, and listen carefully — if they hesitate or default to "operator error," you've learned more than any performance curve could tell you.
Finally, tie the conversation to measured downtime categories rather than overall equipment effectiveness. Ask for the mean time between interventions for each subsystem, and what a typical recovery procedure looks like at 2 a.m. with a junior technician on shift. The answers will reveal whether the line's true capability lives in the engineering design or only in the sales presentation.
Precision You Can Measure: Tolerance Checks Before Signing
Numbers don't lie, but they only tell the truth when the measuring stops. Before any sign-off, every critical dimension gets pulled from the print and checked against the real part sitting on the bench. Calipers click, micrometers settle into place, and a height gauge traces the exact profile that a drawing promised. It's not about trusting the machine or the machinist — it's about verifying the physical reality, one datum at a time.
Tolerance stacking is where quiet failures hide. A bracket that fits in isolation can bind when it meets its mating face, because five tiny deviations added up to a problem nobody saw on paper. That's why the pre-signing check isn't a single pass; it's a sequence of targeted measurements on the features that actually locate, fasten, or seal. If a bore runs to the high side and the pin runs to the low side, that clearance shrinks fast. Spotting that before the ink dries saves a rework loop later.
The real discipline is writing down what you find. A measurement that isn't recorded might as well not exist. Tolerance sheets get filled with as-measured values, not just pass-fail checkmarks, so anyone who signs knows exactly how close the part sits to the edge of its allowed range. That record becomes the backbone of the approval — a fingerprint of the component's geometry at the moment it earned a signature.
Layout Flexibility: Will Their Line Fit Your Floor or Fight It?
Layout flexibility is where a collection either earns its place or becomes a constant compromise. Some lines arrive with a fixed footprint—specific corner configurations, fixed depths, or modular pieces that only work in one direction. If your room has an awkward pillar, a sloped ceiling, or an open-plan flow that doesn’t follow a standard rectangle, those pieces will push back. You end up rearranging your life around the furniture instead of the other way around.
That’s why it pays to look past the showroom setup. A truly adaptable line lets you swap orientations, add or drop sections, and rework the arrangement without needing a custom order or a saw. Ask whether the connectors are reversible, whether the chaise can move from left to right, and whether the pieces can stand alone if your layout changes down the road. If the answer is a shrug or a ‘maybe,’ treat that as a warning.
Floor space isn’t just about measurements—it’s about how a piece behaves in real rooms. A sofa that hugs the wall in one home might block a walkway in another. The best lines don’t fight the floor; they give you enough give-and-take to make the room work, even when the walls aren’t cooperating.
What the Quote Doesn't Show: Energy and Maintenance Realities
A quote can look tidy on a spreadsheet, but it rarely accounts for the month-to-month drain of energy consumption. Two machines with the same purchase price may have very different appetites for electricity, compressed air, or water. If one unit runs hotter or cycles more often, the utility bills start to diverge quickly—and that gap compounds over the equipment’s service life. Buyers who compare only upfront figures often end up paying for the difference every billing cycle without realizing it.
Maintenance expenses hide in similar ways. A quoted price might include basic installation, but it says nothing about how often seals, filters, belts, or software updates will need attention. Some designs use proprietary parts that carry a hefty markup and long lead times. Others demand more frequent calibration or specialized technician visits. Those costs are real and recurring, yet they rarely appear on the first page of a proposal. Asking for a year-by-year operating estimate—not just the purchase number—tends to expose the fuller picture.
Support After Handover: The Difference Between a Partner and a Seller
Once the contract is signed and the initial setup is done, many vendors quietly step back. A true partner, though, treats the handover as the starting line, not the finish. You'll notice it in small ways: they check whether your team actually adopted the new workflow, they flag issues before you discover them on a busy Monday, and they don't charge you for every question that follows.
The practical difference often shows up in how problems are handled. A seller might point to the scope of work and ask for a change order when something breaks or needs adjusting. A partner is more likely to say, Let's figure out what went wrong first, then offer a fix without making you feel like a line item. That shift from transactional to relational support is what keeps implementations from going stale.
Over time, the distinction becomes even clearer. Sellers optimize for the renewal date; partners optimize for your outcomes. If your team gets a new hire or your priorities shift, a partner will help you reconfigure or train rather than disappearing until the next upsell opportunity. That's the kind of continuity that turns a vendor relationship into something you actually rely on.
Longevity Clues: Learning from Existing Bead Wire Lines
Older bead wire lines rarely fail without warning. Maintenance logs from the last fifteen years show that the first signs of trouble almost always appear in the same places—accumulator tension arms, payoff reel brakes, and the bronze coating bath. Operators who track these small drifts catch most problems before they reach the wire drawing dies. That pattern repeats across plants, which suggests longevity depends less on the original equipment than on how quickly teams respond to early friction changes.
Another useful clue comes from comparing two lines built in the same year. One still runs close to its original speed with only routine bearing swaps; the other has been rebuilt twice. The difference is not age but the way each line handles spool changes and wire tension peaks. The longer-lived line consistently avoids rapid acceleration after a splice, while the rebuilt one was pushed harder during shift changes to recover lost time. That small operational habit appears to matter more than any single component upgrade.
Material condition also tells a story worth listening to. Bead wire that passes through older lines often shows faint chatter marks from worn capstans, yet those marks do not always predict early failure. What predicts trouble is a gradual rise in lubricant temperature combined with a drop in coating thickness. Existing lines that get regular thermal scans and coating weight checks tend to outlast those that only get repairs after a visible defect. Longevity clues are already embedded in the daily numbers if the team chooses to read them.
FAQ
Look beyond the price tag. A supplier's engineering track record with similar tire plants, their ability to match your existing wire diameter and ring OD tolerances, and how they handle tension control during winding often matter more than the initial quote.
Ask for a detailed cycle time breakdown rather than just a brochure number. Request references from plants running the same ring sizes and watch a live demonstration if possible. Pay attention to how the line handles acceleration, deceleration, and splice consistency.
At minimum, they should offer remote diagnostics, a local or regional spare parts hub, and training for both operators and maintenance staff. Check their average response time for critical failures and whether they provide documented preventive maintenance schedules.
If your production mix includes frequent size changes or special rubber compounds, yes. Automated quick-change systems for bead ring diameter and width can cut downtime significantly. But if you run long batches of one or two sizes, a simpler, more robust line may be the smarter investment.
Energy consumption, compressed air usage, and consumable wear parts like winding heads or guides are often underestimated. Ask for a realistic cost-per-ring calculation including maintenance labor and spare part replacement intervals over the first five years.
Their engineers should ask about your rubber compound, wire coating, and curing process before quoting. If they talk about bead ring ovality, splice strength, and material handling without being prompted, that's a good sign. Also check whether they've integrated with existing rubber extruders or wire calenders before.
It's becoming a bigger factor. Modern lines with regenerative drives and optimized heating zones can lower operating costs by 15-20% compared to older designs. Ask for specific energy consumption data at your expected throughput, not just peak power ratings.
Very important. A plant visit lets you see how the line handles real production stress, dust, and operator interaction. You can also speak directly with maintenance teams about recurring issues and actual uptime, which is more reliable than a polished sales presentation.
Conclusion
Before you accept any supplier's pitch for a bead wire ring production line, push past the glossy brochure. Ask for actual production logs from recent installations, not just theoretical cycle times. Request a tolerance study using your own compound samples—check not only the average ring diameter but also the scatter across a full shift. A line that holds ±0.1 mm in a demo may drift when run at speed with hot wire. Layout matters just as much: get a scaled footprint drawing, mark your column positions, crane reach, and floor load limits. Some machines demand a pit or special foundation that the quote omits. If the supplier cannot explain how the line will move through your existing doorways or where the scrap bin will sit, keep looking.
Operating cost hides in plain sight. Ask for a real utility bill from a reference customer—compressed air, chilled water, and peak electrical draw often exceed the brochure figures. Maintenance intervals should be stated in hours, not vague "low maintenance" promises. After handover, the difference between a partner and a seller emerges fast: will they stock critical spares locally, offer remote diagnostics, and send a technician without a six-week lead time? Finally, visit a bead wire line that has run for five years or more. Look at wear on guides, bearing housings, and the ring former. Ask the operator what they would change. Those details tell you more about longevity than any warranty clause.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/